Manufacturing companies, CNC operators, engineering workshops, and machining professionals rely on cutting tools to perform drilling, milling, threading, and other metalworking operations.
Dormer Pramet is a recognised cutting-tool brand offering solutions for industrial machining applications.
Hard Metal Traders provides Pakistani businesses with access to industrial tooling options and helps customers inquire about cutting tools suited to their machining requirements.
Dormer Pramet Products for Industrial Applications
Drilling tools
Drilling tools are used to produce holes in metal components, machine parts, and industrial workpieces. Selecting the correct drill depends on the workpiece material, hole depth, diameter, and machining conditions.
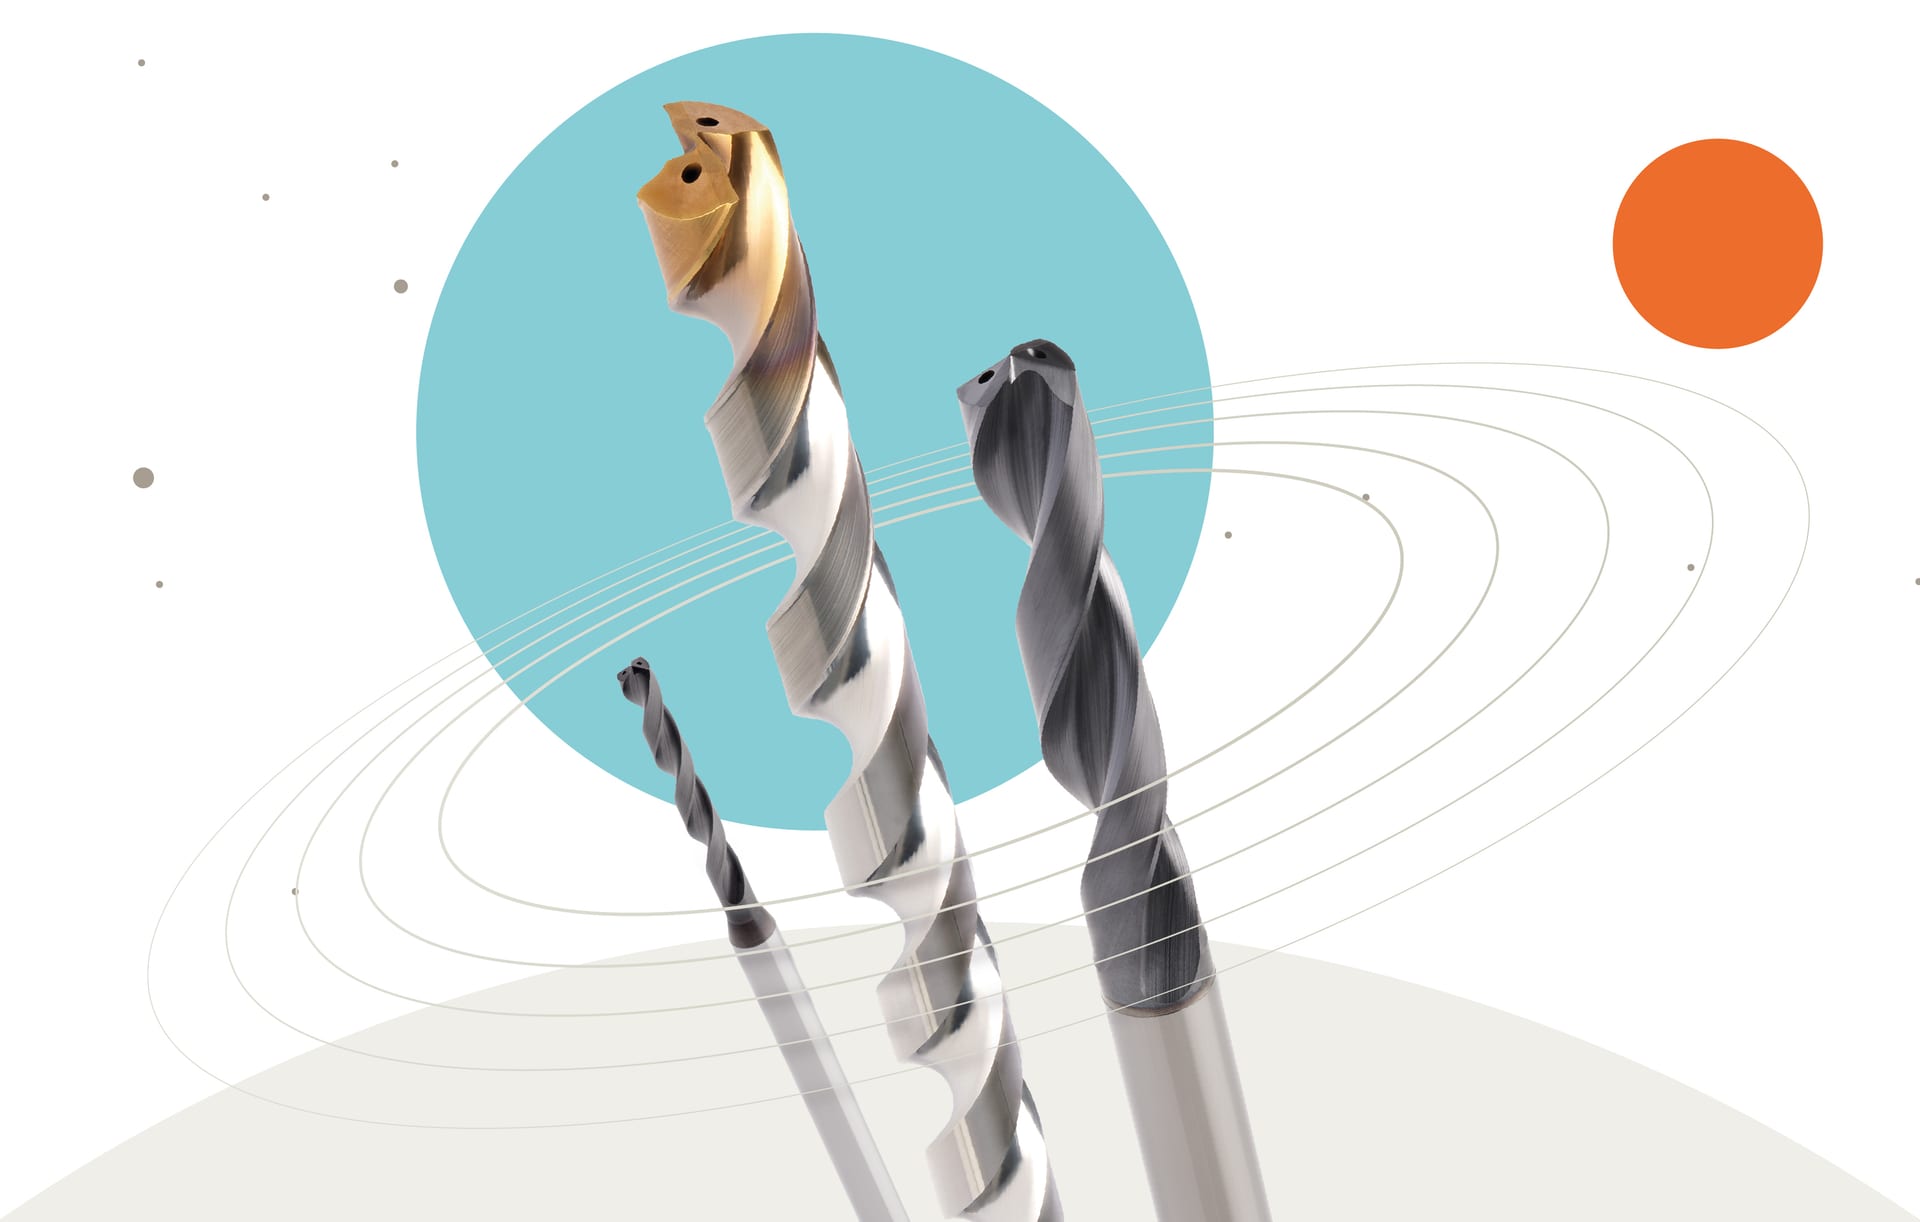 Dormer Pramet Force X Solid Carbide Drill
 Dormer HSS Twist Drills
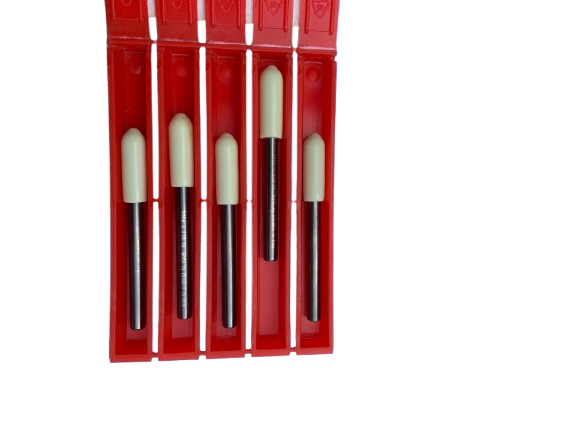
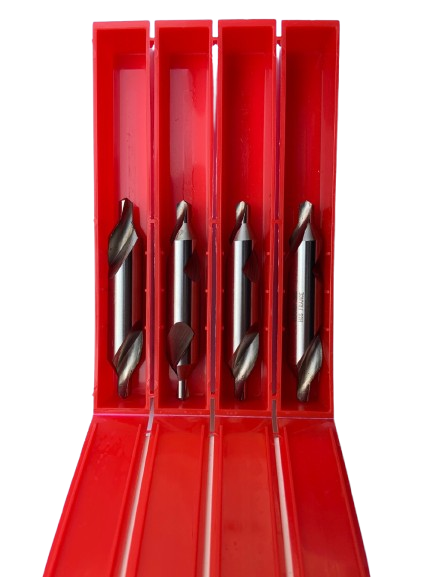 Centre Drills
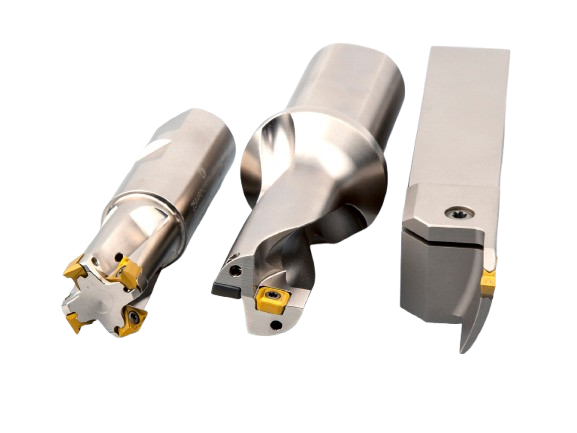 U-Drills and Parting Tool Holders
Milling tools
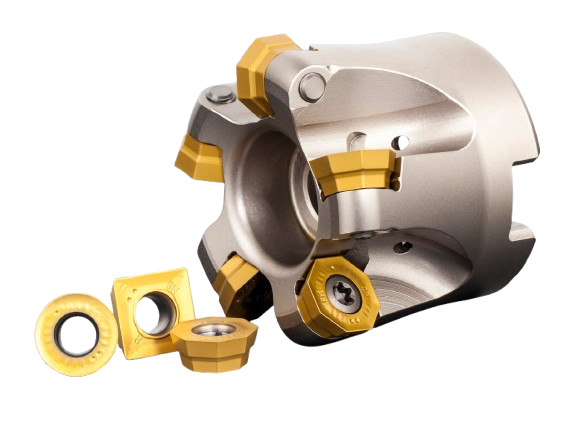
Milling tools are used for machining surfaces, slots, profiles, and other features in metal components. The appropriate tool depends on the material and machining operation.

Turning and threading tools
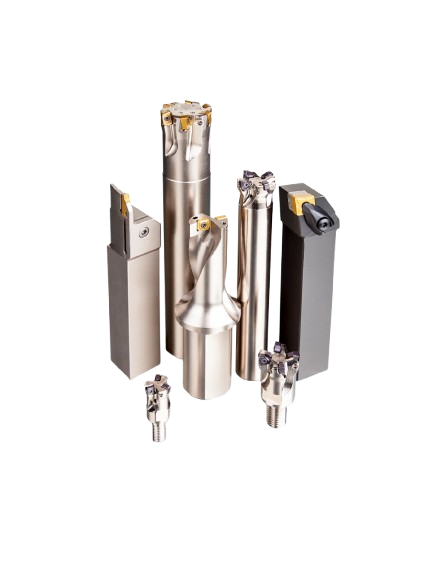
Turning and threading tools are used in machining operations to produce cylindrical surfaces, threads, and precision components.
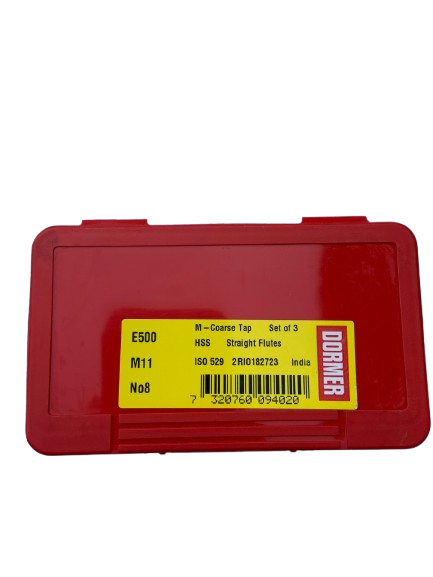
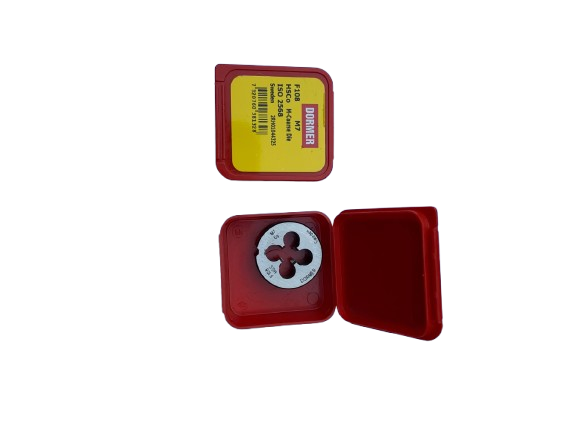
Businesses should confirm the exact tool specification and compatibility before placing an order.
Need a price on a specific tool?
Send the product name, model number and quantity to our team in Lahore. We will come back to you with availability and a quotation.
Where Are Dormer Pramet Cutting Tools Used?
Dormer Pramet cutting tools may be relevant to:
- CNC machining and manufacturing facilities.
- Automotive and engineering workshops.
- Metal fabrication and component production.
- Industrial maintenance and machining operations.
For businesses in Lahore, Karachi, Faisalabad, Gujranwala, Sialkot, and other industrial locations in Pakistan, sourcing suitable tooling is an important part of maintaining production operations.
Common Machining Problems and What They Usually Point To
Before replacing a tool with a different brand, it is worth checking whether the tool is the actual problem. Most premature failures trace back to a handful of causes.
| What you are seeing | Most likely cause | What to change first |
|---|---|---|
| Cutting edge wears evenly but very fast | Cutting speed too high for the material, or insufficient coolant | Reduce surface speed before changing tool grade |
| Edge chips or fractures | Interrupted cut, vibration, or a carbide tool in a setup that is not rigid enough | Check workholding and overhang; consider a tougher grade or cobalt HSS |
| Built-up edge, poor surface finish | Cutting speed too low, or the wrong geometry for a sticky material | Increase speed, or move to a sharper, more positive geometry |
| Drill wanders off centre | No spot or centre drill, worn point, or an unequal point grind | Spot the hole first and check the point angle symmetry |
| Tap breaks or produces oversized threads | Wrong tapping drill size, poor alignment, or swarf packing in a blind hole | Verify the tapping drill diameter and use a spiral flute tap for blind holes |
If none of these apply, send us the tool designation and a description of the failure and we will help work through it.
Thinking in Cost Per Hole, Not Cost Per Tool
The purchase price of a cutting tool is often the smallest part of what it costs you. A drill that costs several times more but produces many times more holes before regrinding, at a higher feed rate, is usually cheaper in practice once machine time and tool changes are counted.
The figures worth tracking are simple: how many parts the tool produced, how long the cut took, and how many minutes of machine time each tool change consumed. Once you have those for your current tool, comparing a alternative becomes an arithmetic question rather than a matter of opinion.
This matters most on high-volume work. For maintenance and one-off jobs, availability and breadth of sizes usually beat marginal gains in tool life.
Spiral Flute, Spiral Point or Straight Flute Taps?
Thread tapping fails more often than any other operation in a general workshop, and the flute form is usually the deciding factor.
- Spiral point (gun) taps push swarf forward, ahead of the tap. They suit through holes and are the most robust choice where the chip can escape.
- Spiral flute taps pull swarf back out of the hole. They are the right answer for blind holes, where a packed chip is what breaks the tap.
- Straight flute taps are the general-purpose option, and are well suited to hand tapping and short-chipping materials such as cast iron.
Getting the tapping drill diameter right matters just as much. Aiming for full thread depth in steel is a common and expensive mistake, as the extra engagement adds torque without adding meaningful strength.
Buy Dormer Pramet Cutting Tools in Pakistan
Hard Metal Traders is a Lahore-based industrial tools supplier. Contact our team to inquire about Dormer Pramet products, specific tool requirements, current availability, and pricing.